
Custom CNC Machining Parts Manufacturer in Dongguan China
China
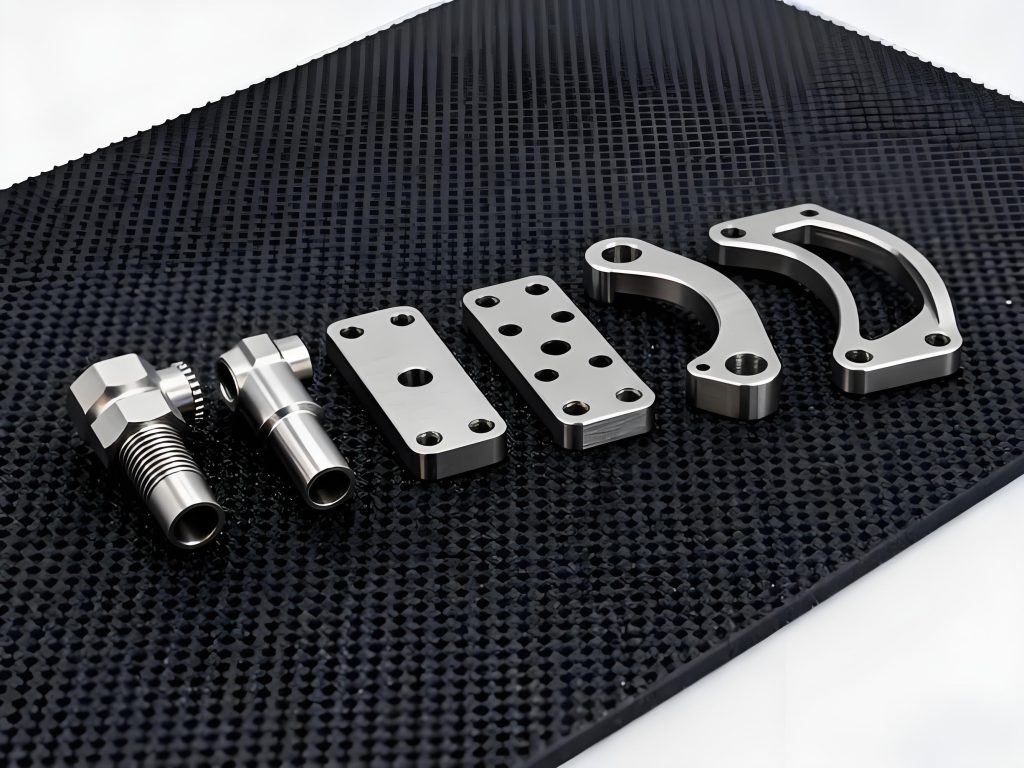
You’ve spent months perfecting a design. It’s lightweight, highly integrated, and geometrically optimized for performance. But when you send the drawing to your local machine shop, the response is discouraging: “We can’t hold those tolerances with multiple setups,” or worse, “We don’t have the capability to machine this at all.”
This is the reality for many engineers working on next-generation products — from surgical robots and satellite communications payloads to advanced automotive powertrains and semiconductor wafer-handling systems. The more you optimize a design for performance, the more complex the geometry becomes. And the fewer suppliers can actually make it.
The good news? A specialized tier of Chinese CNC manufacturers has turned 5-axis machining from a “premium luxury” into a production-ready, cost-effective daily operation. If you can’t find a shop that can handle your intricate components, it’s time to look at what Chinese 5-axis experts are doing — because they’re likely already producing parts just like yours, at scale, with documented quality.
This article explains what makes a part truly “complex,” why traditional shops struggle, how Chinese suppliers overcome those barriers, and how to identify a partner who can actually deliver.
What Makes a Part “Too Complex” for Most Shops?
Complexity in CNC machining isn’t just about the number of features. It’s about geometric inaccessibility and tolerance interdependence across multiple axes. Here’s what typically pushes a part beyond what a standard 3-axis shop can handle:
| Complexity Factor | Why It’s Difficult | Typical Failure Mode |
|---|---|---|
| Compound-angle holes | Require angled fixtures or EDM; each re-fixturing adds ~0.015–0.03mm cumulative error | Hole position drifts out of true position tolerance |
| Deep ribbed pockets | Aspect ratios >4:1 require long-reach tooling, which deflects and chatters | Poor surface finish, dimensional drift, broken tools |
| Freeform / sculpted surfaces | Tool must maintain optimal contact angle across continuously changing geometry | Stair-stepping, gouging, or excessive hand polishing |
| Thin-walled sections (<1.5mm) | Part deflects under cutting forces; residual stress causes springback after unclamping | Flatness and profile tolerances cannot be held |
| Multi-sided features with cross-axis datums | Datum references span three or more faces at different orientations | CMM inspection fails on positional callouts |
| Tight tolerances across split lines | Features machined in separate setups must align perfectly | Mating parts don’t fit; assembly interference |
If your part checks two or more of these boxes, you need a 5-axis shop. Not a 3-axis shop with a rotary table bolted on — a shop that lives and breathes simultaneous 5-axis machining.
Why 3-Axis and 4-Axis Fall Short
A 3-axis VMC can only approach the part from the top and four sides (via manual re-fixturing). Every time an operator unclamps, rotates, and reclamps the part, three things happen:
-
Locating error is introduced. Even with precision vises and dowel pins, a re-clamp shifts the part by 5–20 microns.
-
Setup time multiplies. Each new setup requires fresh CAM, new fixtures, and new inspection planning.
-
Scrap risk compounds. A single crash or misalignment in setup #4 ruins a part that was perfect through setups #1–3.
A 4-axis indexer helps — it adds one rotary axis — but it’s still fundamentally positional. You can’t tilt the tool to follow a curved surface or reach into a deep pocket at an angle. For true geometric complexity, you need simultaneous 5-axis: three linear axes (X/Y/Z) plus two rotary axes (A/B or B/C) moving together in a single toolpath.
The 5-Axis Advantage — And Why Chinese Suppliers Excel at It
What Simultaneous 5-Axis Actually Delivers
| Capability | Impact on Complex Parts |
|---|---|
| Single-setup completion | Eliminates cumulative locating error; all critical datums machined in one clamping |
| Shorter, stiffer tools | By tilting the tool to the surface normal, you can use a short tool even in a deep cavity — no deflection, no chatter |
| Optimal tool-to-surface engagement | Tool axis continuously adjusts to maintain ideal stepover and cutting speed, producing superior surface finish (often Ra 0.4–0.8 µm as-machined) |
| Undercut and deep-pocket access | Tilting the head allows the tool to reach behind features and into recesses impossible on 3-axis |
| Reduced EDM dependency | Many internal corners and deep slots that would require sinker EDM can be roughed and finished with lollipop cutters on 5-axis |
The Chinese 5-Axis Ecosystem
China isn’t just “catching up” in 5-axis machining — in many segments, it’s operating at global parity. Here’s what the top tier looks like:
Machine Tools (Common in Leading Chinese Facilities):
-
DMG Mori DMU 50 / 65 / 85 monoBLOCK — simultaneous 5-axis, thermal compensation, < 0.005mm positioning accuracy
-
Hermle C 22 / C 32 / C 42 — German-built, renowned for rigidity and volumetric accuracy; widely used in Chinese aerospace and medtech shops
-
Mazak VARIAXIS j-500 / i-700 | — high-speed 5-axis, integrated rotary table, excellent for aluminum and titanium
-
Grob G350 / G550 — swivel-head design, exceptional for complex die/mold and structural components
-
GF Machining Solutions Mikron MILL P 500 / 800 U — purpose-built for high-precision 5-axis production
CAM Software & Programming:
-
Open Mind hyperMILL — industry-leading 5-axis simultaneous strategies, automatic collision avoidance
-
Mastercam Multiaxis — widely used, strong for impellers and porting
-
Autodesk PowerMill — strong for complex surface machining and electrode work
-
Siemens NX CAM — full CAD/CAM integration, common in aerospace-tier suppliers
Tooling & Workholding:
-
HSK-A63 / HSK-A100 tool holders — high-speed, high-rigidity clamping with low runout (< 0.003mm)
-
Zero-point clamping systems (Schunk Vero-S, Erowa) — 0.002mm repeatability for quick changeovers
-
Hydraulic expansion tool holders — superior damping for thin-wall finishing passes
The Labor Factor:
China produces thousands of CNC programmers annually who specialize in multi-axis machining. The talent pool is deep, and the programmers working at top-tier export-focused shops have often cut hundreds of complex parts across industries. They’re not learning on your job — they’ve already solved your problem on someone else’s part six months ago.
Case Study: Surgical Robot Articulating Arm Segment
Part specifications:
-
Material: Titanium Grade 5 (Ti-6Al-4V), AMS 4928
-
Dimensions: 145 × 88 × 62 mm
-
Key challenges:
-
1.2mm wall thickness on curved sections (risk of vibration and springback)
-
Five-sided machining with 18 compound-angle mounting holes
-
True position ±0.008mm on all hole patterns relative to a 3-datum structure
-
Surface finish Ra 0.8 on all external contours (no hand polishing allowed)
-
-
Quantity: 80 pieces (first production batch)
-
End use: Articulated link in a laparoscopic surgical robot arm
Why a 3-Axis Shop Couldn’t Do It
A US-based 3-axis shop quoted the part with seven separate setups. Their DFM feedback noted:
-
“We can’t hold ±0.008mm true position across 7 setups — expect ±0.025mm at best.”
-
“Thin walls will chatter; we recommend increasing to 2.5mm.”
-
“Lead time: 6–8 weeks. Cost: ~$420/part.”
The design team couldn’t compromise on wall thickness (weight budget) or tolerances (bearing preload requirements).
How the Chinese 5-Axis Supplier Executed It
| Step | Process Detail |
|---|---|
| Machine | DMG Mori DMU 65 monoBLOCK, simultaneous 5-axis |
| CAM | hyperMILL 5-axis simultaneous; trochoidal roughing to minimize heat and stress |
| Workholding | Custom aluminum soft jaw, machined to match part contour; zero-point quick-change base |
| Roughing | Trochoidal toolpaths with through-spindle coolant (70 bar); 6mm carbide end mill, leaving 0.4mm stock on all walls |
| Stress relief | 12-hour rest at 20±1°C between roughing and finishing |
| Finishing | 4mm ball nose, simultaneous 5-axis flow machining; surface finish achieved Ra 0.6–0.8 µm |
| Hole making | All 18 compound-angle holes drilled and reamed in the same setup using 5-axis positioning; Renishaw probe verified each hole location before machining |
| Inspection | Zeiss Contura CMM; full FAI with ballooned drawing; SPC on 10% of production parts |
| Result | 98% yield; all critical features within ±0.006mm; Cpk = 1.71 |
| Cost | ~$185/part (including anodizing and DDP shipping to the US) |
Bottom line: The Chinese 5-axis shop delivered a part the US 3-axis shop said was “not feasible as drawn” — at 56% lower cost and in half the lead time (18 days vs. 6–8 weeks).
How to Vet a True 5-Axis Supplier
Not every shop with a “5-axis CNC” sign on the door can actually deliver intricate components. Here’s how to separate the real experts from the pretenders:
The Capability Audit
| What to Ask | What a Real Expert Says | Red Flag |
|---|---|---|
| “Do you run simultaneous 5-axis or just 3+2 positional?” | “Both. We use simultaneous for freeform surfaces and 3+2 for indexed hole patterns.” | “We mostly do 3+2. Simultaneous is too slow.” |
| “What CAM software do your programmers use?” | Names specific software (hyperMILL, PowerMill) and can describe their 5-axis strategies | “We use the built-in CAM in our CAD software” |
| “Can you show me a complex part you’ve machined?” | Sends photos + CMM report of a part with compound curves or deep ribs | Sends photos of simple aluminum brackets |
| “What tool holding system do you use?” | HSK, BIG-PLUS, or hydraulic chucks; mentions runout tolerance | “Standard CAT40/BT40 collets” |
| “Do you have on-machine probing?” | Yes, Renishaw or Blum; describes how they use it for in-process verification | “We inspect after machining at the QC bench” |
| “What’s your scrap rate on 5-axis jobs?” | Gives a real number (e.g., 2–4%) and explains how they track it | “We never scrap parts” (impossible at micron levels) |
The “Test Feature” Challenge
Include one intentionally tricky feature in your RFQ — for example, a deep pocket (depth = 5× width) with a 3mm fillet radius at the bottom corner and a compound-angle hole intersecting the side wall. A shop that quotes it without comment probably doesn’t fully understand what they’re bidding on. A real 5-axis expert will respond with a specific machining strategy: “We’ll use a 6mm lollipop cutter for the corner fillet and approach the side hole at 35° using simultaneous 5-axis positioning. Tool length will be 48mm max to avoid deflection.”
That level of specificity is your green light.
DFM Tips for 5-Axis Parts: Designing for the 5th Axis
You can make your supplier’s life — and your own cost structure — dramatically better with a few design choices:
1. Design for Single-Setup Machining
Group critical features so they can all be accessed from one clamping. If your datum structure requires three faces at 90° to each other, that’s perfect for 5-axis — all three can be machined in one setup by tilting the table.
2. Avoid “Impossible” Internal Corners
In a deep pocket, the cutter must fit both the depth and the corner radius. A 2mm corner radius in a 40mm-deep pocket requires a 4mm cutter sticking out 42mm — it will deflect or break. Either:
-
Increase the corner radius (3mm minimum for that depth)
-
Use a lollipop cutter (adds cost but feasible)
-
Accept that EDM might be needed (adds lead time)
3. Specify Realistic Surface Finish
A simultaneous 5-axis finish pass can achieve Ra 0.4–0.8 µm on sculpted surfaces without hand polishing. But if you call out Ra 0.2 µm, you’re asking for manual super-finishing or abrasive flow machining — massive cost and time additions.
4. Use Draft Angles on Deep Ribs
Even on 5-axis, a 1°–2° draft on deep thin walls allows the tool to clear chips more effectively and reduces cutting forces. Your part stays truer to tolerance.
5. Call Out Only What Matters
If a non-critical face has a profile tolerance of ±0.05mm, don’t call out ±0.01mm. Every tight tolerance on a 5-axis part adds inspection time and scrap risk. Let the supplier put their effort where it counts.
Common Complex Parts Chinese 5-Axis Shops Excel At
| Industry | Part Type | Why 5-Axis Is Essential |
|---|---|---|
| Medical | Surgical instrument handles, implant trials, robotic end-effectors | Biocompatible materials (Ti, CoCr), organic shapes, no hand-finishing allowed |
| Aerospace | Brackets, housings, ducting components | Thin-wall aluminum, tight positional tolerances, multi-directional features |
| Semiconductor | Wafer-handling end effectors, vacuum chambers, gas distribution blocks | Aluminum 6061/7075, extreme flatness, complex internal channels |
| Automotive / EV | Electric motor housings, brake caliper prototypes, sensor brackets | High mix, low volume, tight deadlines |
| Industrial / Robotics | Joint housings, lightweight structural arms, custom gearboxes | Organic shapes for weight reduction, multi-axis hole patterns |
| Marine / Energy | Impellers, pump volutes, valve bodies | True 5-axis simultaneous required for bladed geometries |
The Bottom Line
If you’ve been told your part is “too complex” or “can’t be machined as designed,” don’t redesign your product around your supplier’s limitations. The right 5-axis shop can make it happen — and Chinese suppliers with deep 5-axis expertise are doing it every day for companies around the world.
The key is finding a partner who combines the right hardware (machines, probing, tooling), the right software (hyperMILL, PowerMill), and — most importantly — programmers and machinists who have already solved the exact problems your part presents.
Your next step: Pull the most geometrically challenging part from your current project. Send the STEP file and 2D drawing to three Chinese suppliers who advertise 5-axis capability. In your RFQ, ask one specific question: “What is your proposed machining strategy for the compound-angle features on this part?” The depth and specificity of their answer will tell you everything you need to know.

No reply content