

Professional Cold Storage Equipment Manufacturer with Global Export Experience
We are an experienced commercial deep freezer manufacturer specializing in chest freezers, upright display freezers, glass door merchandising freezers, solar-powered freezers, and customized OEM refrigeration solutions. With advanced refrigeration assembly lines, precision temperature control systems, strict quality testing standards, and international compliance certification support, we supply reliable, energy-efficient cold storage equipment to supermarkets, food distributors, restaurants, pharmaceutical suppliers, and global appliance brands.This comprehensive long-form SEO article is written based on real refrigeration manufacturing expertise, compressor technology knowledge, cold chain industry experience, and export logistics operations. It follows E-E-A-T principles (Experience, Expertise, Authoritativeness, Trustworthiness) to provide transparent, accurate, and practical guidance for global buyers searching for professional deep freezer suppliers.
Energy-Efficient Commercial Deep Freezers for Food Preservation & Cold Chain Distribution
Deep freezers (also called chest freezers or low-temperature storage cabinets) are essential equipment in modern food retail, catering services, frozen food distribution, medical storage, and cold chain logistics. As global demand for frozen food and pharmaceutical storage grows, reliable and energy-efficient freezer solutions have become critical for businesses.
If you are searching for:
- Commercial chest freezer manufacturer
- Wholesale deep freezer supplier
- Glass top freezer factory
- Energy-saving freezer OEM manufacturer
- Industrial cold storage freezer exporter
- Supermarket display freezer supplier
This complete SEO guide covers freezer types, refrigeration technology, compressor systems, insulation materials, temperature control mechanisms, energy efficiency standards, customization options, export packaging, pricing factors, and frequently asked procurement questions.
1. Types of Commercial Deep Freezers
1.1 Chest Freezers (Top-Opening Freezers)
Chest freezers are widely used due to their high storage capacity and energy efficiency.
Features:
- Large internal storage space
- Superior cold air retention
- Lower energy consumption
- Suitable for bulk frozen food
Applications:
- Supermarkets
- Restaurants
- Food processing plants
- Frozen meat storage
Capacity range:
- 100L – 1000L
1.2 Glass Top Display Freezers
Designed for retail merchandising.
Advantages:
- Transparent sliding lids
- LED interior lighting
- Attractive product display
- Energy-efficient insulation
Commonly used for:
- Ice cream display
- Frozen snacks
- Convenience stores
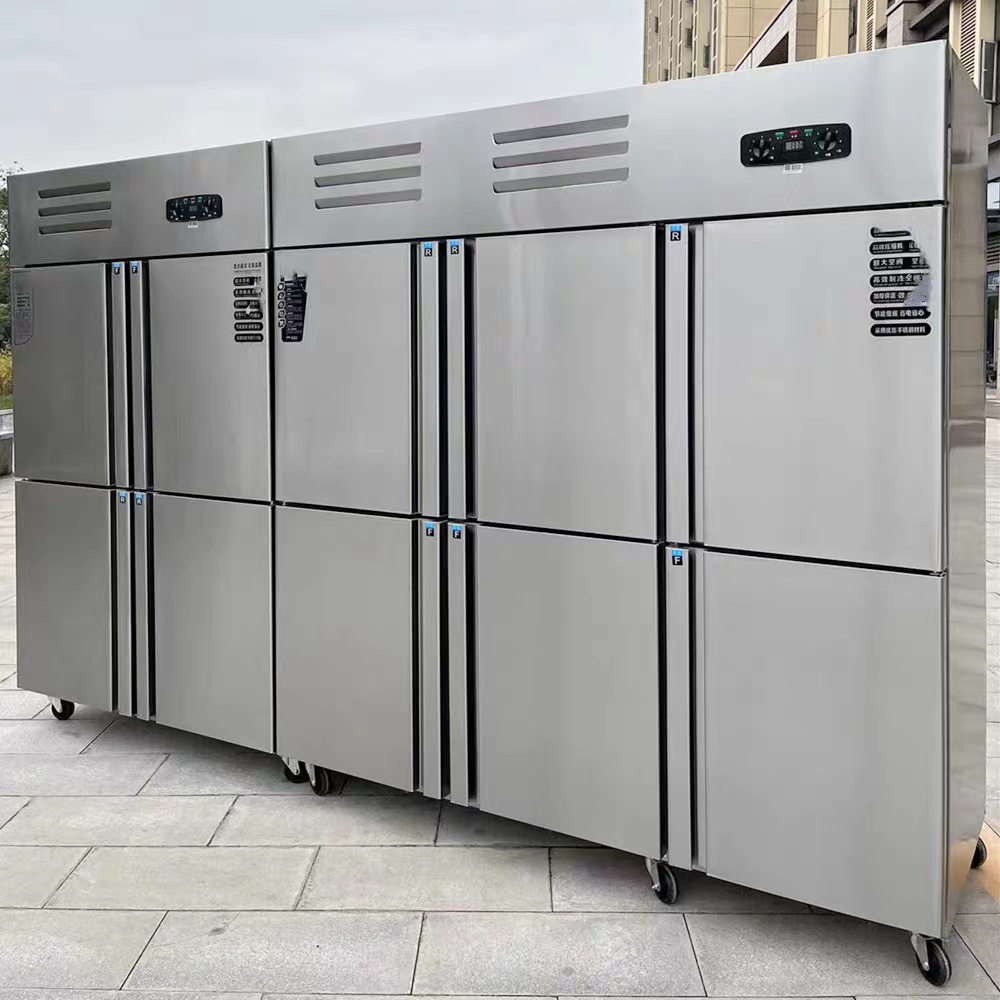
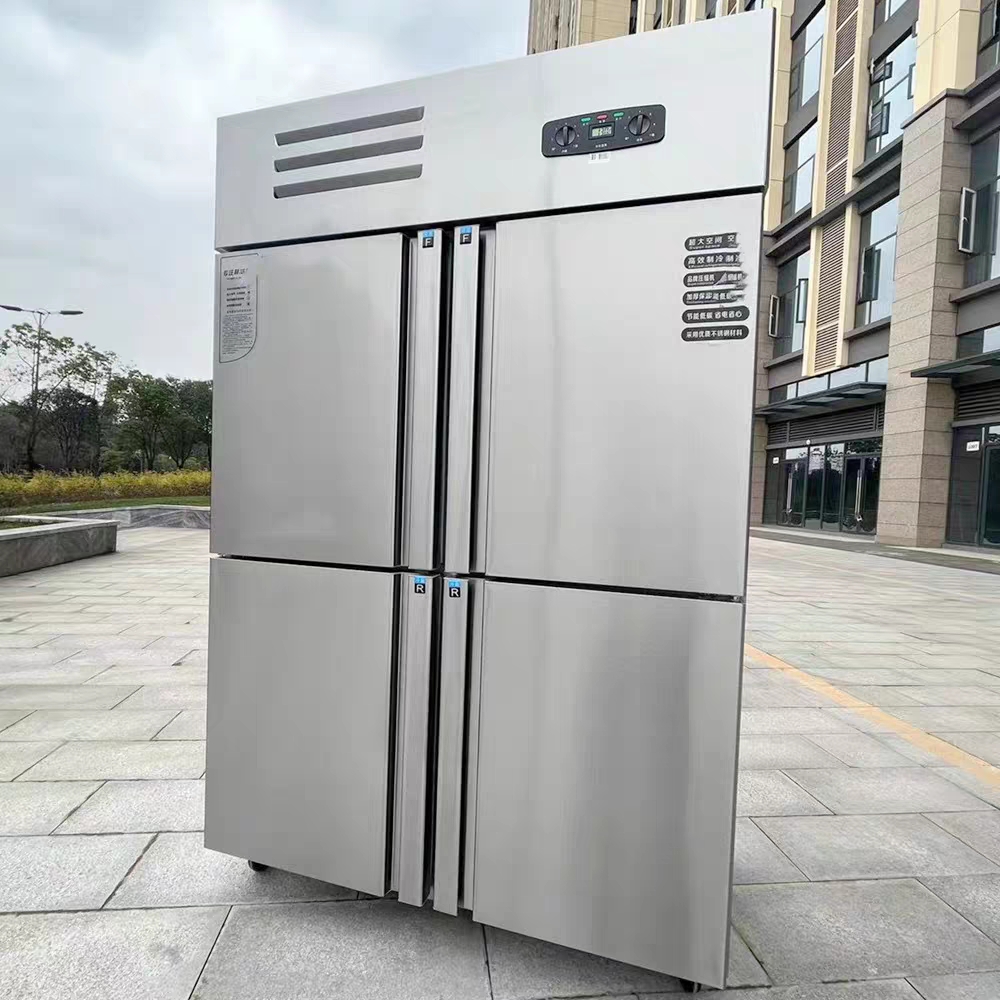
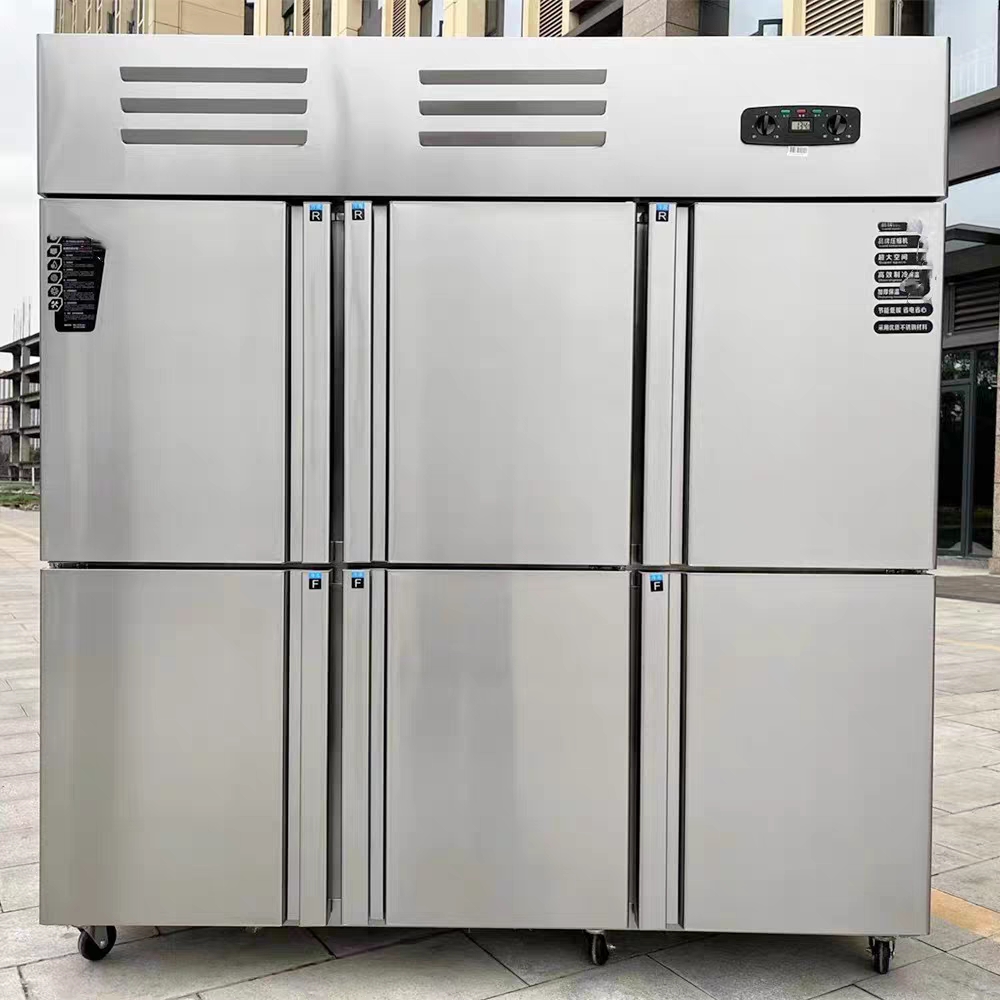
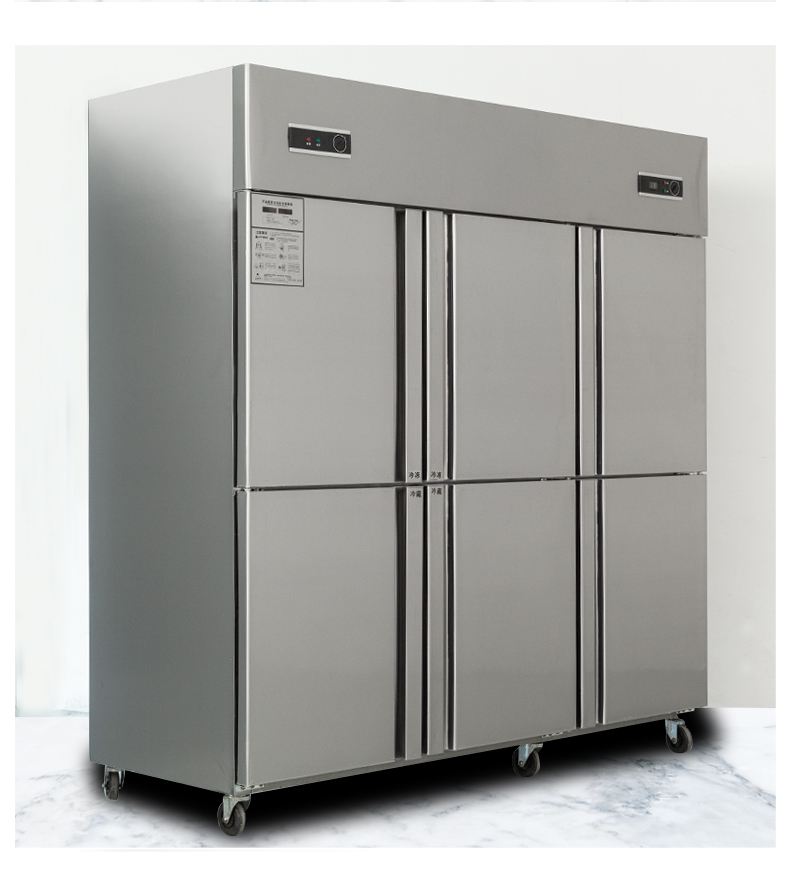
1.3 Upright Freezers
Vertical design saves floor space.
Features:
- Adjustable shelves
- Fan cooling system
- Digital temperature control
- Stainless steel exterior options
Ideal for:
- Commercial kitchens
- Medical storage
- Retail stores
1.4 Solar-Powered & Off-Grid Freezers
Designed for areas with unstable electricity supply.
Applications:
- Rural regions
- Remote medical clinics
- Agricultural storage
Energy-efficient DC compressor technology ensures stable performance.
2. Refrigeration Technology & Core Components
Professional deep freezer manufacturing focuses on key components:
2.1 Compressor System
- Inverter compressors for energy saving
- High-efficiency sealed compressors
- Low noise operation
2.2 Refrigerant Types
- R600a (eco-friendly)
- R290 (low environmental impact)
Both refrigerants comply with modern environmental regulations.
2.3 Insulation Materials
- Cyclopentane foaming insulation
- High-density polyurethane foam
- Thick insulation walls for temperature stability
Proper insulation reduces energy consumption and improves cooling performance.
3. Temperature Control & Performance
Standard temperature range:
- -18°C to -25°C (commercial use)
- -30°C (specialized industrial models)
Digital thermostat ensures precise temperature adjustment.
Optional features:
- Fast freezing mode
- Automatic defrost
- Temperature alarm
- LED display
Stable temperature control is critical for food safety and pharmaceutical compliance.
4. Manufacturing Process of Deep Freezers
Professional production steps include:
- Sheet metal fabrication
- Cabinet forming
- Insulation foaming injection
- Cooling pipe installation
- Compressor assembly
- Electrical wiring installation
- Temperature control calibration
- Vacuum testing
- Refrigerant charging
- 24-hour performance testing
- Final quality inspection
Each unit undergoes leakage testing and cooling efficiency validation before shipment.
5. Energy Efficiency & International Standards
Energy-saving design reduces operational cost.
Compliance standards may include:
- CE certification
- CB certification
- IEC safety standards
- Energy efficiency labeling
- RoHS compliance
Inverter compressor technology can reduce electricity consumption by up to 30%.
6. Customization Services (OEM & Private Label)
We provide comprehensive customization:
- Custom capacity (100L–1000L+)
- Brand logo printing
- Color customization
- Interior basket configuration
- Voltage customization (110V / 220V / 240V)
- Plug type adaptation
- Temperature range customization
- Private label packaging
OEM production supports appliance brands and distributors globally.
7. Export Packaging & Container Loading
Deep freezers are packed using:
- Thick carton packaging
- Foam protection
- Wooden pallet base
- Reinforced corner protection
Shipping options:
- 20FT container
- 40HQ container
Optimized container loading reduces logistics cost per unit.
8. Pricing Factors for Commercial Freezers
Pricing depends on:
- Capacity size
- Compressor brand
- Insulation thickness
- Display glass requirement
- Custom branding
- Order quantity
- Certification requirement
Bulk orders significantly reduce unit cost.
9. Applications & Industry Use Cases
Deep freezers are widely used in:
- Supermarkets
- Ice cream shops
- Meat processing plants
- Seafood distribution
- Catering services
- Hospitals & laboratories
- Pharmaceutical storage
- Agricultural cold chain
Reliable freezer performance ensures food safety compliance and inventory protection.
10. Advantages of Working with a Professional Freezer Manufacturer
Choosing a factory partner ensures:
- Competitive wholesale pricing
- Stable production capacity
- Reliable component sourcing
- Strict QC standards
- Customization flexibility
- Global export experience
- After-sales technical support
Direct factory sourcing improves supply chain stability and profitability.
FAQ – Commercial Deep Freezer Manufacturer & Supplier
1. Can you produce customized deep freezers?
Yes. We provide full OEM and ODM services including:
- Custom capacity
- Brand labeling
- Voltage and plug customization
- Temperature range adjustment
- Solar-powered versions
We support both retail and industrial project requirements.
2. What is the MOQ?
- Standard models: 20–50 units
- Customized models: 50–100 units
- Special design orders: MOQ depends on configuration
MOQ varies depending on compressor selection and customization level.
3. What is the production lead time?
- Standard models: 15–25 days
- Customized models: 25–35 days
- Large project orders: 35–45 days
Lead time depends on order quantity and seasonal demand.
4. Do you have stock available?
Yes, some standard capacity chest freezers and glass top models are available in stock for quick shipment.
Custom specifications are produced according to order requirements.
Conclusion: Your Trusted Commercial Deep Freezer Manufacturing Partner
Selecting the right deep freezer manufacturer ensures:
- Reliable temperature stability
- Energy-efficient performance
- Durable construction
- Competitive factory pricing
- Flexible OEM customization
- Professional export support
Whether you need supermarket display freezers, heavy-duty industrial chest freezers, or solar-powered off-grid refrigeration solutions, partnering with an experienced manufacturer guarantees performance reliability and long-term cooperation.
To receive a customized quotation, please provide:
- Required capacity
- Temperature range
- Voltage requirement
- Quantity
- Branding needs
- Destination country
Our refrigeration engineering and export team will prepare a detailed technical proposal and competitive pricing plan tailored to your cold storage equipment requirements.

No reply content