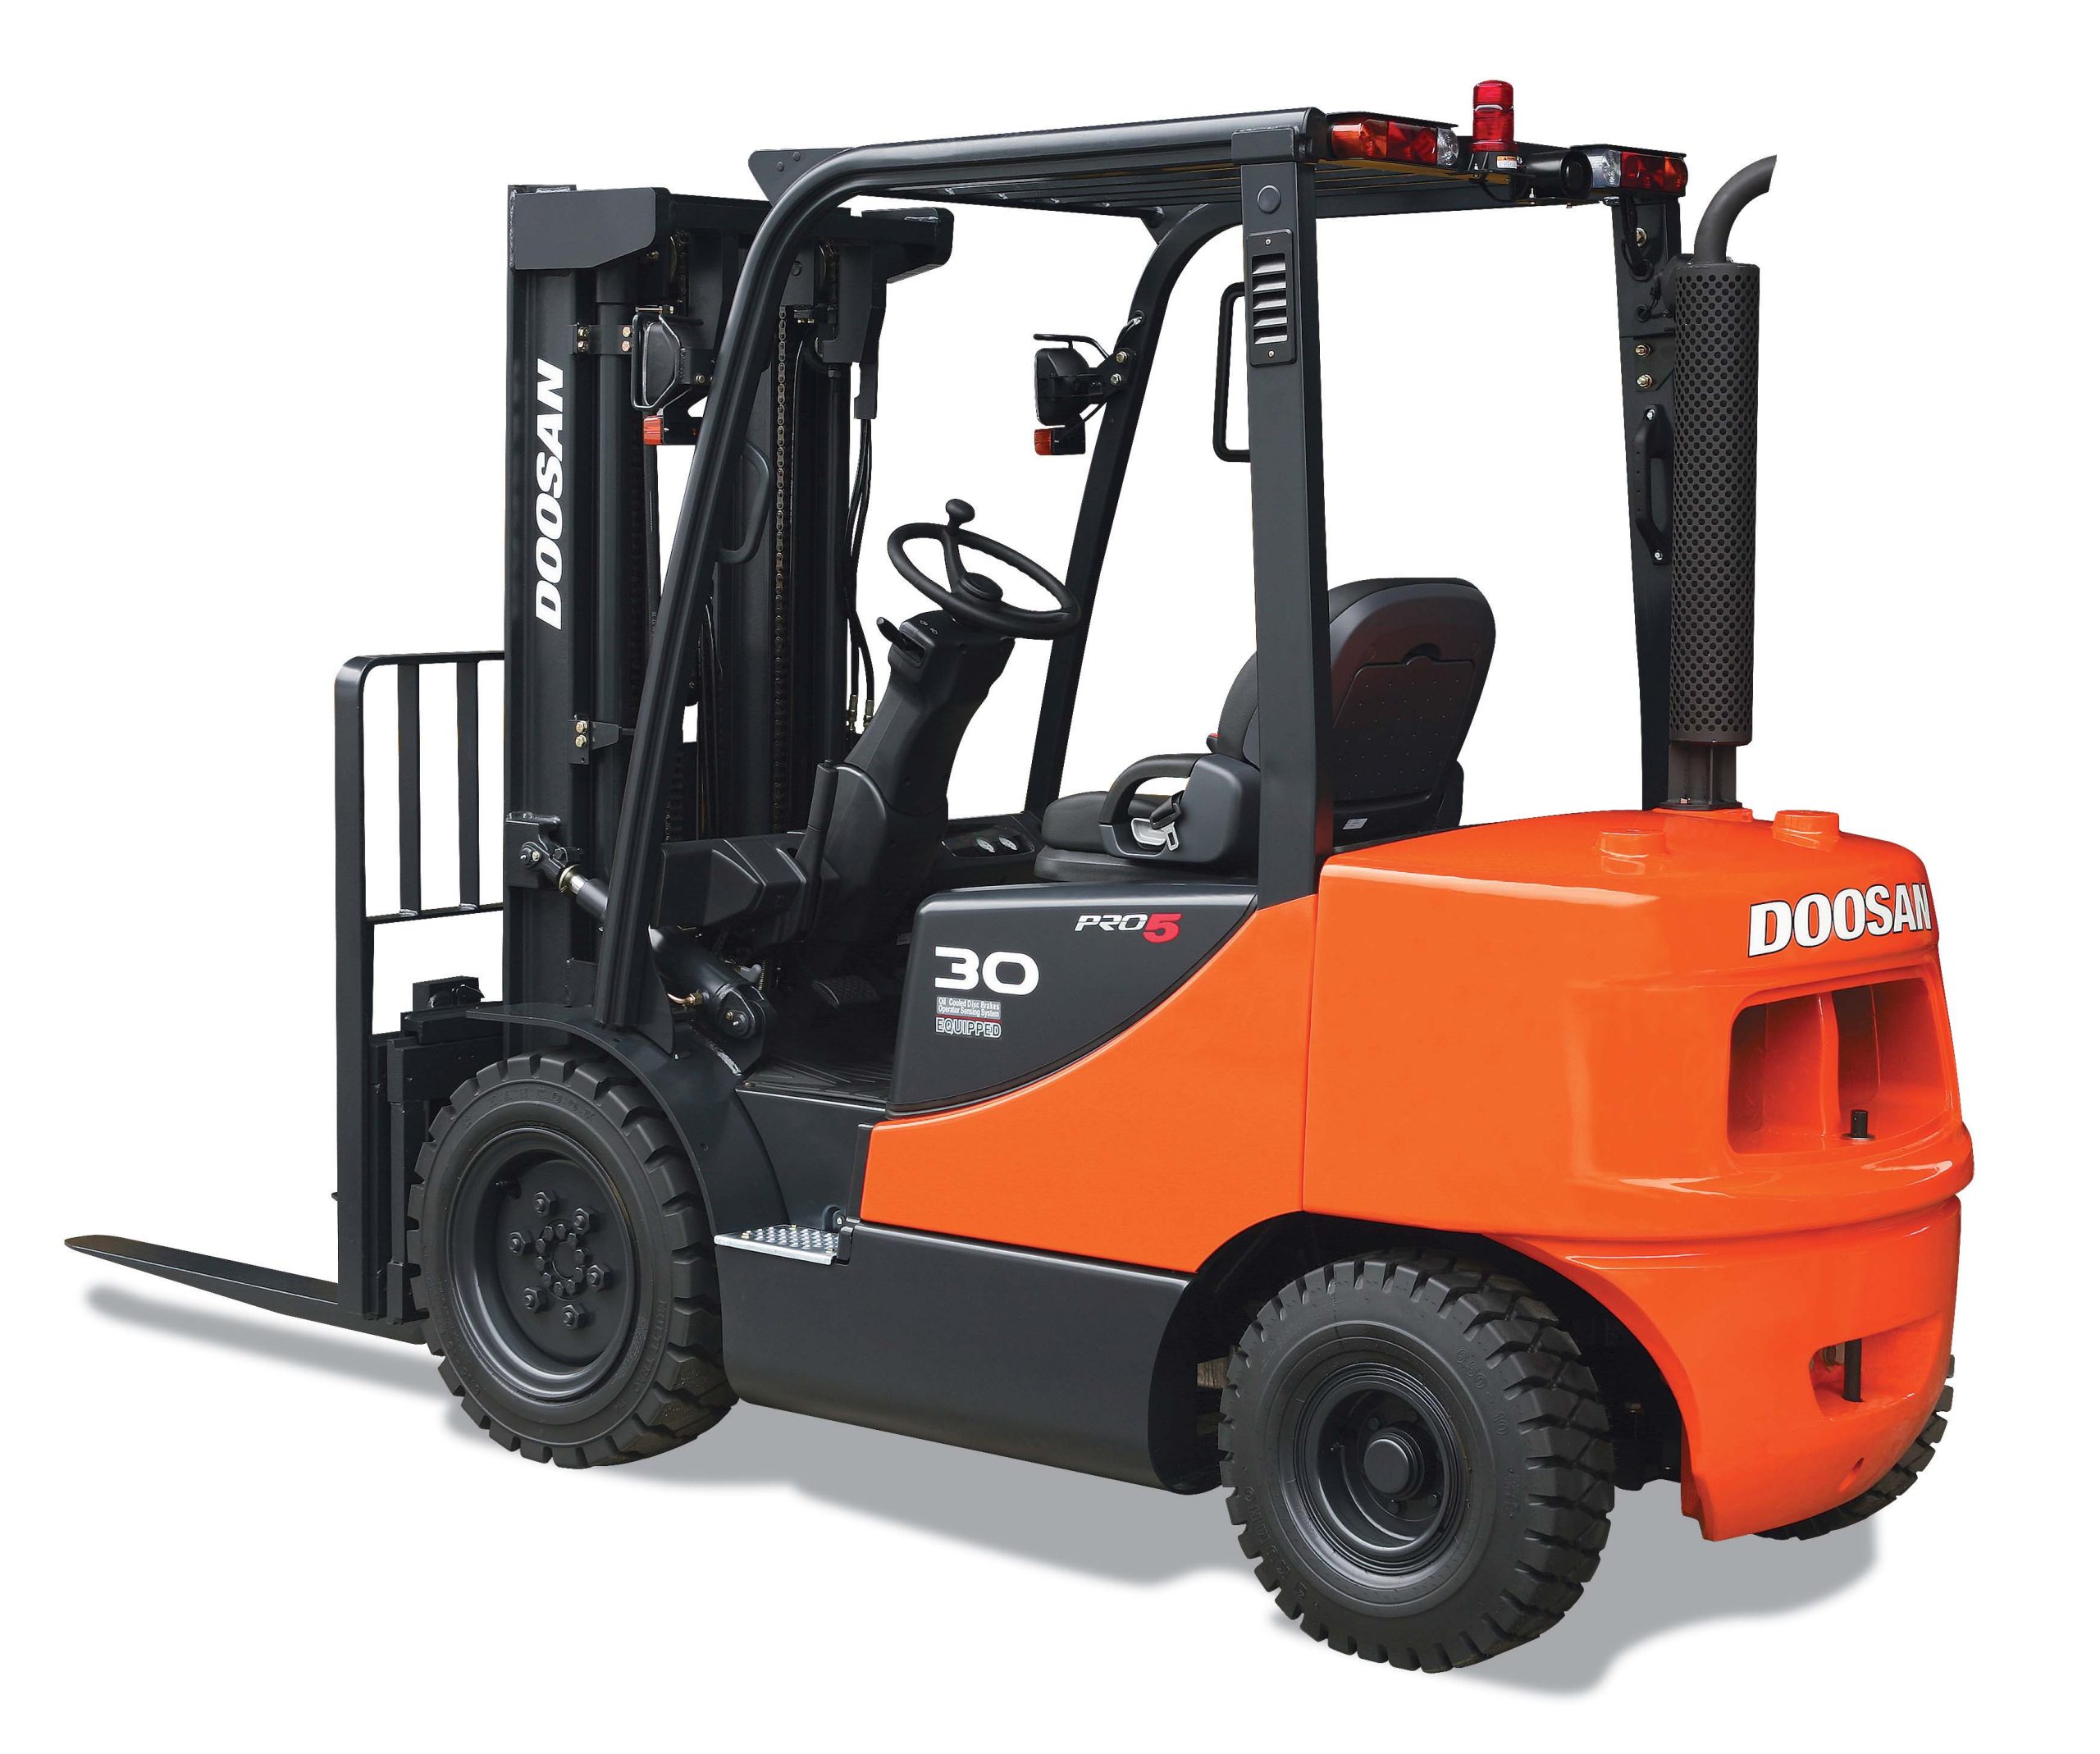
Guangzhou Forklift Manufacturing Factory
It’s 2:30 p.m. on a Friday. Your busiest shipping day of the week. Three orders are staged and ready to load, and a fourth just came off the production line. Then the horn sounds—the one everyone in the warehouse dreads. Your lead forklift operator is standing next to a dead truck, the hydraulic lift is stuck at 12 feet, and a $40,000 pallet of product is suspended over an aisle with nowhere to go.
You call your dealer. The earliest a technician can show up is Tuesday. The repair quote, once it finally arrives, is $4,800—for a truck you bought 18 months ago.
If this scenario feels familiar, you’re not alone. Unplanned forklift downtime costs the average warehouse $2,000–$5,000 per incident when you factor in lost productivity, emergency service calls, expedited parts, and delayed shipments. Over a 5-year lifespan, a “budget” forklift with chronic reliability issues can quietly drain $60,000–$100,000 more than a properly engineered truck.
The frustrating part? It’s almost entirely preventable.
As a direct forklift manufacturer supplying electric pallet jacks, counterbalance trucks, reach trucks, and narrow-aisle equipment to warehouses and distribution centers across 40+ countries, we’ve engineered our designs around one non-negotiable principle: uptime is everything. In this guide, we’ll break down exactly why standard off-the-shelf forklifts fail prematurely—and how manufacturer-grade engineering can push your fleet past 10,000 hours of reliable operation.
The Real Cost of a “Cheap” Forklift
Most procurement teams buy forklifts the way they buy fleet vehicles: compare upfront sticker prices, pick the lowest bidder, and move on. But a forklift isn’t a delivery van—it’s a piece of continuous-use industrial equipment that operates 6–10 hours a day in harsh conditions. And when it goes down, your entire operation stops with it.
What You See
|
What It’s Actually Costing You
|
Truck down for 2 days waiting for a part
|
2 operators idle × $22/hr × 16 hrs = $704 in labor waste
|
Emergency weekend service call
|
$800–$1,500 in overtime technician fees
|
Delayed outbound shipment
|
$2,000–$10,000+ in penalty clauses or lost customer goodwill
|
Load stuck on a raised mast
|
Safety hazard—potential OSHA citation or injury claim
|
Premature engine/transmission failure at 3,000 hrs
|
$8,000–$15,000 in replacement cost (vs. expected 10,000 hr life)
|
🔑 The kicker: A forklift that costs $18,000 upfront but breaks down 4 times a year is significantly more expensive than a $26,000 truck that runs flawlessly for 5 years. Yet most RFPs still rank bids by purchase price alone.
Why Do Standard Forklifts Fail So Fast?
Before we talk solutions, let’s diagnose the root causes. After servicing thousands of units in the field, here are the five failure points that account for 80% of all forklift downtime:
1. Hydraulic System Leaks and Pump Failures
The hydraulic system is the heart of any forklift. Cheap seals, undersized pumps, and poor filtration cause pressure drops, slow lifting, and eventually complete system failure. Once hydraulic fluid contaminates the mast channels, you’re looking at a full rebuild.
2. Transmission and Drive Train Wear
In internal combustion (IC) trucks, transmissions take the brunt of stop-start warehouse traffic. In electric trucks, drive motor brushes wear out prematurely when motors aren’t properly sealed against dust and debris.
3. Battery Degradation (Electric Models)
Lead-acid batteries in budget electric forklifts typically last 1,000–1,500 charge cycles—about 3–4 years of single-shift use. But improper charging habits, lack of watering systems, and thermal runaway can cut that to 18 months. When the battery dies, the truck is a $20,000 paperweight.
4. Mast and Carriage Metal Fatigue
The mast is a welded steel structure subjected to constant cantilever stress. Inferior steel grades, poor weld penetration, and inadequate gusseting lead to micro-cracks that eventually propagate into visible fractures—especially at the weld joints connecting the inner and outer mast channels.
5. Electrical Harness and Controller Failures
Modern forklifts are packed with sensors, controllers, and CAN-bus systems. Cheap wiring harnesses with poor weatherproofing (IP54 instead of IP65+) corrode quickly in humid or cold-storage environments, causing intermittent faults that are a nightmare to diagnose.
How Direct Manufacturers Engineer 10,000+ Hour Uptime
Here’s where buying factory-direct changes the game. When you source through a dealer network, you’re buying a truck that was spec’d to hit a target price point for the dealer’s margin. When you work directly with the manufacturer, you can spec a truck engineered for total cost of ownership.
1. Reinforced Chassis and Mast Construction
The foundation of forklift reliability is structural integrity. Direct manufacturers with in-house fabrication control every weld:
-
High-tensile steel (Q345/St52.3) for mast channels—30% higher yield strength than standard mild steel
-
Robotic welding with 98%+ penetration rates (vs. manual welding with inconsistent penetration)
-
Full gusset plates at all high-stress joints (mast-to-carriage, overhead guard mounts)
-
Shot-blasted and powder-coated frames resist corrosion 3× longer than liquid paint
🔑 Pro tip: Ask for the mast steel grade specification. If your supplier can’t tell you the exact steel grade and weld standard (e.g., ISO 3834), they’re not controlling structural quality tightly enough.
2. Japanese and EU-Sourced Core Components
Smart manufacturers don’t build everything in-house—they integrate the best components from global suppliers. Here’s what to look for:
Component
|
Budget Spec
|
Manufacturer-Grade Spec
|
Hydraulic pump
|
Generic Chinese gear pump
|
Shimadzu (Japan) or Bucher (Switzerland) vane pump
|
Drive motor
|
Brushed DC motor
|
AC induction motor (brushless, 30% longer life)
|
Controller
|
Basic Curtis 1200 series
|
Curtis 1230/1380 series or Zapi (Italy) with diagnostics
|
Hydraulic valves
|
Standard directional valve
|
Monoblock valve with load-holding check valves
|
Tires
|
Solid pneumatic (cheap compound)
|
Polyurethane (electric) or premium solid (IC) with wear indicators
|
🔑 Pro tip: A forklift is only as reliable as its weakest component. A world-class mast with a generic hydraulic pump will still leave you dead on the floor. Insist on a full component list before you buy.
3. Lithium-Ion Battery Technology (The Game Changer)
If you’re still running lead-acid electric forklifts, you’re managing a high-maintenance liability. Lithium iron phosphate (LiFePO₄) batteries are transforming forklift uptime:
Feature
|
Lead-Acid Battery
|
Lithium-Ion (LiFePO₄)
|
Cycle life
|
1,000–1,500 cycles
|
3,000–5,000 cycles
|
Charge time (0–100%)
|
8–10 hours + cool-down
|
1.5–2 hours (opportunity charging OK)
|
Maintenance
|
Weekly watering, equalizing
|
Zero maintenance
|
Energy efficiency
|
60–70%
|
95%+
|
Replacement cost (5-year)
|
$3,500–$6,000
|
$0 (battery outlasts truck)
|
Cold storage performance
|
Loses 30–40% capacity at 0°C
|
Operates at full capacity to -20°C
|
🔑 Pro tip: Lithium forklifts cost 15–25% more upfront but eliminate battery maintenance labor, watering stations, and mid-shift battery swaps. For multi-shift operations, the payback period is typically 12–18 months.
4. IP65+ Sealed Electrical Systems
For cold storage, food processing, and outdoor applications, water and dust ingress are the #1 killers of electrical components. Manufacturer-engineered trucks feature:
-
Fully sealed connectors (Deutsch or equivalent IP67-rated)
-
Conformal-coated controller boards resist condensation
-
Weatherproof display panels with membrane switches rated for 1M+ cycles
-
Encapsulated drive motors prevent washdown water from reaching windings
5. Simplified Service Access (Because Maintenance Will Always Be Needed)
Even the best-engineered forklift needs periodic service. The difference is how easy it is to perform:
-
Tilt-out battery compartments for 30-second battery access
-
Removable side panels (no tools required) for daily checks
-
Centralized grease points with extended-service intervals (250 hrs vs. 125 hrs)
-
CAN-bus diagnostics port—plug in a laptop and read fault codes in seconds
The Numbers: Budget Forklift vs. Manufacturer-Engineered Truck
Let’s run a 5-year total cost of ownership (TCO) comparison for a 3,000 kg electric counterbalance forklift running single shift (2,000 hrs/year):
Cost Element
|
Budget Lead-Acid Truck ($16,000)
|
Manufacturer Li-Ion Truck ($22,000)
|
Purchase price
|
$16,000
|
$22,000
|
Battery replacement (Year 3)
|
$4,500
|
$0
|
Battery maintenance labor (5 yrs)
|
$2,800
|
$0
|
Unplanned repairs (avg. per year)
|
$3,200
|
$800
|
Downtime cost (5 yrs @ $2,000/incident)
|
$32,000 (4 incidents/yr × 5)
|
$8,000 (1 incident/yr × 5)
|
Energy cost (5 yrs @ $0.12/kWh)
|
$4,800
|
$3,200 (more efficient)
|
Total 5-Year Cost
|
$63,300
|
$37,000
|
Cost per Operating Hour
|
$6.33/hr
|
$3.70/hr
|
Net savings over 5 years: $26,300 per truck. For a fleet of 10 forklifts, that’s $263,000 back in your pocket.
How to Choose the Right Forklift for Your Operation
Not every warehouse needs the same spec. Here’s the manufacturer’s quick-decision matrix:
Your Operation
|
Recommended Power Type
|
Key Feature
|
Indoor, narrow aisles (<10 ft)
|
3-wheel electric (Li-Ion)
|
1,600–2,000mm turning radius
|
Indoor, wide aisles, heavy loads
|
4-wheel electric (Li-Ion)
|
3,000–5,000 kg capacity
|
Outdoor, rough terrain, yard
|
IC diesel or LPG
|
Pneumatic tires, sealed air intake
|
Cold storage (-20°C to -30°C)
|
Electric Li-Ion (cold-spec)
|
Cold-rated hydraulic fluid, sealed electronics
|
Multi-shift, 24/7 operation
|
Electric Li-Ion (fast charge)
|
Opportunity charging during breaks
|
Food & pharmaceutical
|
Electric (sealed systems)
|
Stainless steel options, easy-clean surfaces
|
Why Manufacturer-Direct Matters for Forklifts
Forklifts are complex machines with 2,000+ components. When you buy through a dealer, you’re adding a markup—typically 25–40%—and inserting a layer of separation between you and the people who actually built the machine.
What You Need
|
Dealer / Distributor
|
Direct Manufacturer
|
Full component specification sheet
|
❌ “Standard OEM parts” (vague)
|
✅ Exact brand/model of every major component
|
Customization (attachments, mast height, tire type)
|
❌ Limited to dealer inventory
|
✅ Built to your spec on the production line
|
Spare parts pricing
|
❌ 100–200% markup on list price
|
✅ Factory cost + shipping
|
Technical support for diagnostics
|
❌ “Call a technician” ($150/hr)
|
✅ Free remote troubleshooting via CAN-bus data
|
Warranty claim processing
|
❌ 2–4 week approval cycle
|
✅ Direct claim, parts shipped in 48 hrs
|
Prototype/special build lead time
|
❌ 12–16 weeks
|
✅ 6–8 weeks (standard), 3–4 weeks (expedited)
|
Stop Letting Breakdowns Dictate Your Schedule
A forklift that spends more time in the repair bay than on the floor isn’t an asset—it’s a liability. The difference between a truck that dies at 3,000 hours and one that’s still running strong at 10,000+ hours isn’t luck. It’s engineering decisions made on the factory floor.
If your current fleet is costing you more in downtime than it’s saving in throughput, it’s time to rethink your sourcing strategy. A manufacturer-direct forklift engineered for uptime isn’t just a purchase—it’s an infrastructure investment.
👉 Get a free fleet assessment and TCO quote from our engineering team. Tell us your application (indoor/outdoor, load weight, daily hours), and we’ll recommend the exact model with a 5-year cost projection—no obligation.
No dealer markup. No upsell. Just straight answers from the people who actually build the trucks.

No reply content